
Efficient steam generation at NÖM dairy
Effective heat recovery with heat exchangers
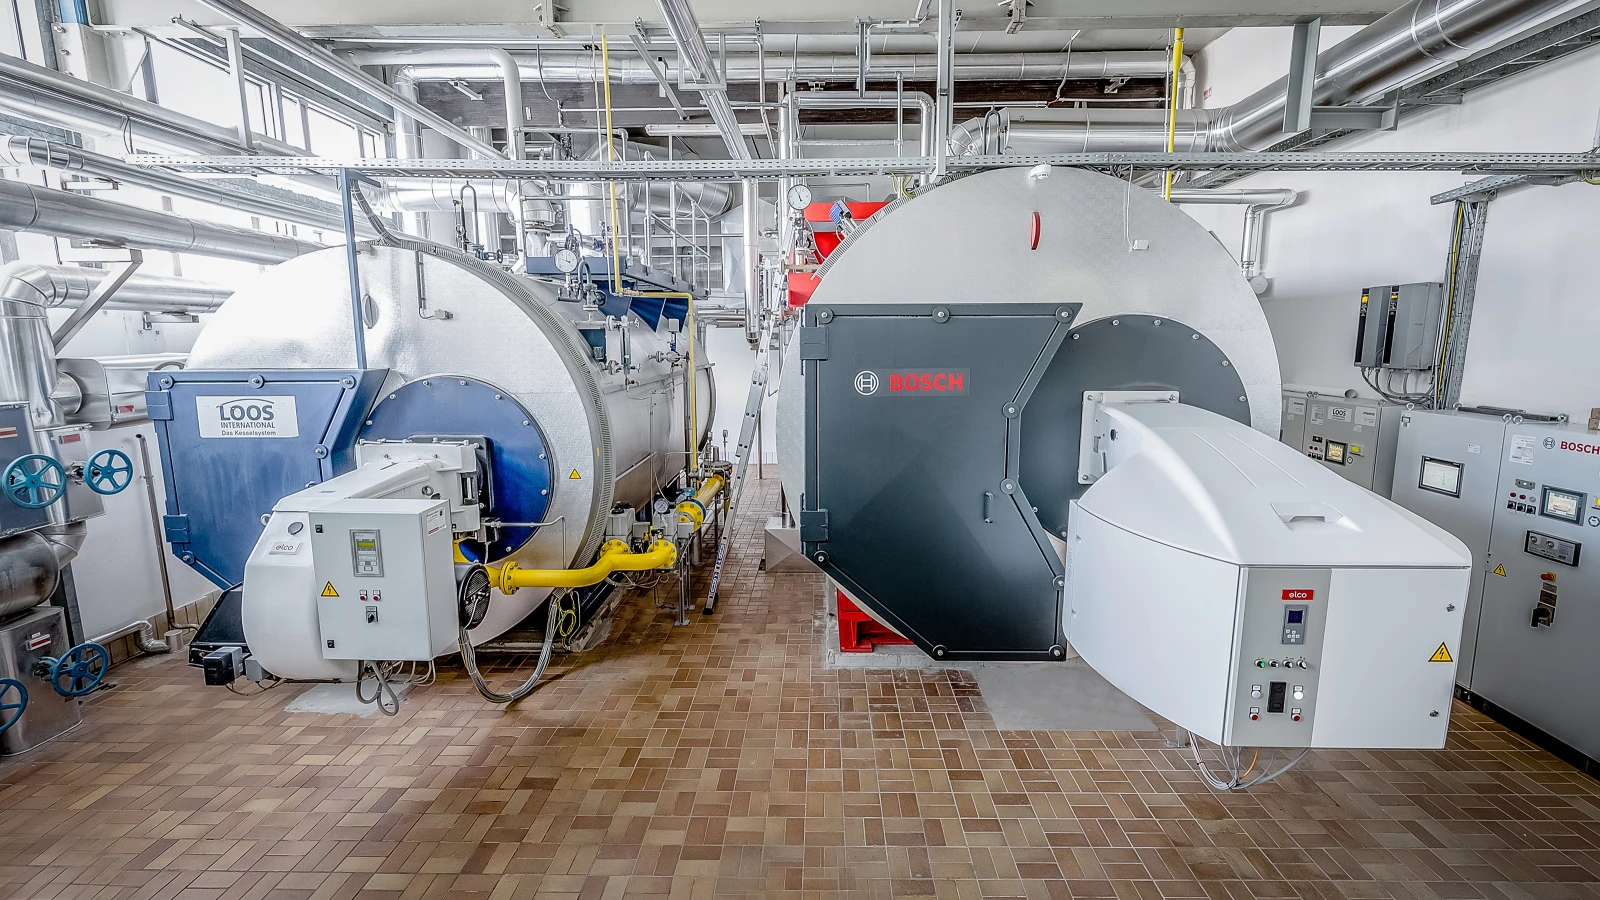
The operator
NÖM AG in Austria has an impressive record with its innovative dairy products for 115 years. It processes some one million litres of milk per day at its factory in Baden, which is located close to the modern and constantly growing city of Vienna. Responsibility, effective environmental conduct and the highest quality aspirations are indispensable to the company. Since 2009 NÖM has been using exclusively 100 percent GM-free milk from 3,200 dairy farms in Lower Austria and the border regions.
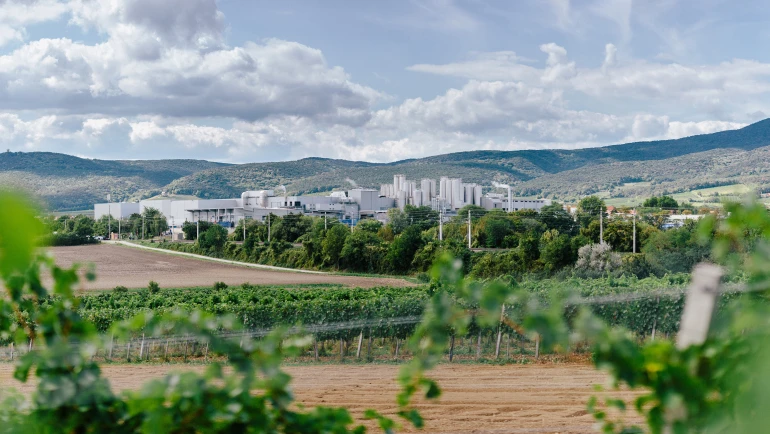
The main factory at NÖM Dairy uses steam for many important production processes such as pasteurisation, sterilisation, cleaning and operating the UHT plants (Ultra High Temperature processing).
The project
In recent years NÖM AG has recorded steady growth and decided to make important and trendsetting investments at its Baden location. In order to be able to process the larger production requirements, the dairy has expanded and modernised the supply of processing heat, which is provided by two steam boilers. One of these boilers had to be replaced with a new and larger steam generator. This came from the Bosch factory in Gunzenhausen (Germany) and can provide up to 14,500 kilograms of steam per hour. A further aim for the company was to achieve the best possible energy efficiency in order to save operating costs and protect the environment. The entire project, from the engineering work through to the automation and right up to the final installation, was carried out by the plant construction company, Edtmayer Systemtechnik GmbH.
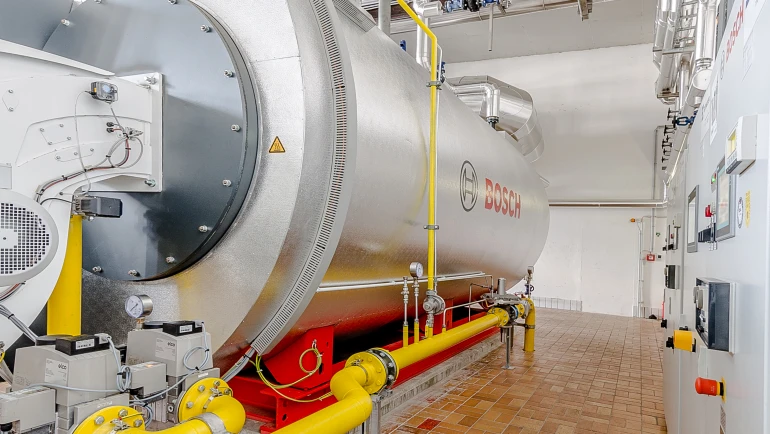
The new Bosch boiler was integrated quickly and efficiently into the existing steam network.
From Loos to Bosch
In 2010 the dairy company had a boiler from Loos (today Bosch) installed with an output of 10,700 kilograms of steam per hour. The installed output of the system was no longer sufficient however, due to company mergers and the resulting higher steam requirement at the Baden location. The Loos boiler now serves primarily as security of supply. It also guarantees uninterrupted production during service and maintenance work on the new steam boiler.
The same type of construction of both boilers enabled the existing feed water treatment module to be integrated easily. Condensate and make-up water flow continuously. After making some appropriate modifications, Edtmayer has also been able to connect the automatic removal and examination of water samples to the existing system. This means that both steam boilers and the feed water module are monitored.
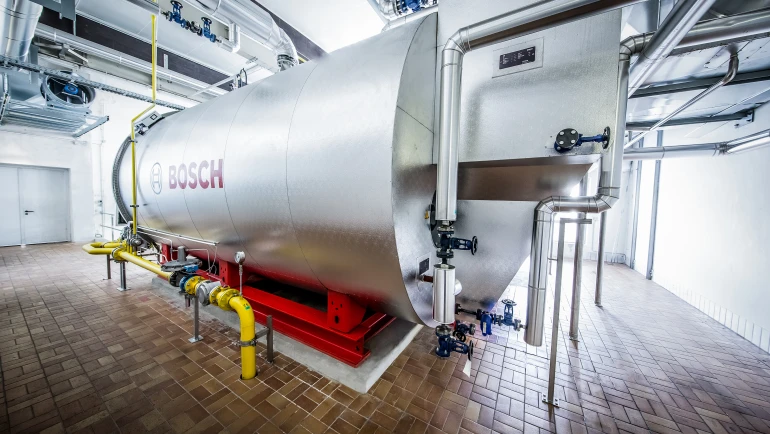
The use of flue gas heat exchangers protects the environment and reduces fuel costs.
Effective heat recovery with two heat exchangers
In order to provide the steam for the dairy company very efficiently, the Bosch boiler is equipped with two flue gas heat exchangers. Using the hot flue gases from the boiler, the integrated economizer preheats the feed water very effectively. This enables fuel usage to be reduced when generating steam, and the flue gas temperature is lowered to 115 °C. The condensation heat from the flue gas is used by the downstream condensate heat exchanger to heat the cold fresh water from 12 to 85 °C. Up to 6,100 litres of water per hour can be heated. The temperature of the flue gas is reduced further and exit with 55 °C. Air contaminants, such as carbon dioxide and nitric oxide, are reduced to a minimum at all operating points.
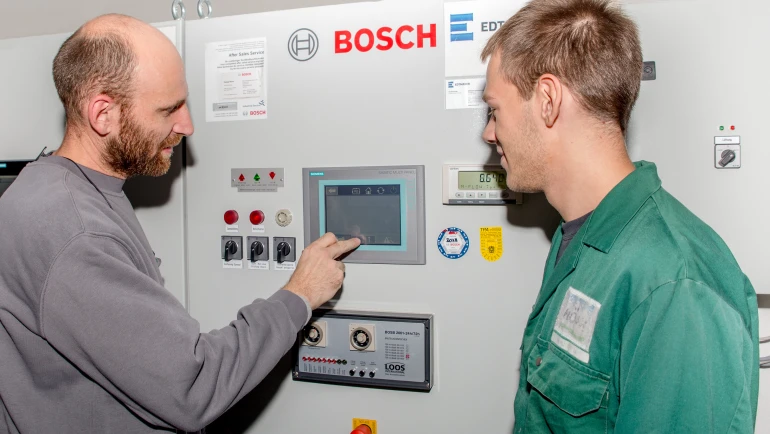
The Bosch controls can be operated intuitively and reduce the need for supervision.
Automation for higher reliability
The boiler control (BOSB 2001-72h) is fully automated and enables the steam boiler to be operated for 72 hours without constant supervision. The integrated Condition Monitoring software supports the operators in running the system efficiently and preventively. It generates maintenance messages for example, or detects desalting rates that are too high. Safety devices protect the boiler against operating errors and, if necessary, switch operation automatically to the back-up boiler. The staff at the dairy are constantly provided with current operating data via the central control system.
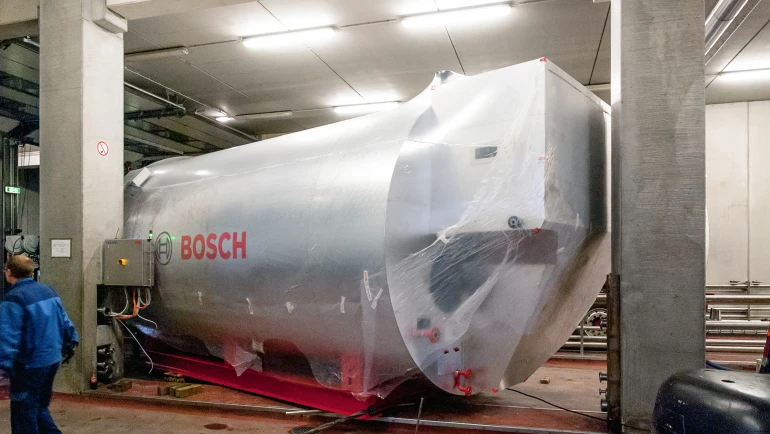
Restricted space conditions demanded a lot of all those involved.
Bringing the boiler into site with precision
Due to restricted space in the buildings at the Baden location, it was a particular challenge for those involved in the project to bringing the boiler into site. The boiler was placed on rollers and manoeuvred through a narrow, 50 metre long passageway towards the boiler house. When it arrived at the hole in the wall, which had been opened up specially, a great deal of skill and a good eye for dimensions were required. The boiler, which measured 7.5 metres long and 3.2 metres wide, was inched between two concrete pillars and then gradually turned into the boiler house. Prior to this, parts of the milk transfer system, as well as railings to the basement floor, had to be dismantled. Some fittings, such as the burner, were also only installed on site due to the restricted space. After ten hours of perfectly coordinated work, the boiler was successfully positioned.
Other special features of the project
-
The site of the new steam boiler was equipped with special foundations due to the basement floor below. It prevents vibrations that are damaging to the boiler, as well as relieving pressure on the ceiling.
-
The integrated heating coils keep the boilers warm, thus enabling to switch immediately to the second boiler if required
-
The modulating burner facilitates flexible operation with low fuel consumption
The result
The new steam boiler system is designed to respond to demand, and it enables milk processing to be performed economically and sustainably. Thanks to effective heat recovery, fuel consumption and CO2 emissions are reduced significantly. The project manager responsible at NÖM Dairy is very satisfied with the realisation.
Bringing the steam boiler into site was a huge challenge for all those involved. But all the effort was worth it however, when one looks at the achieved efficiency of 102.7 percent and the very effective operation of the system. Thanks to the 100-percent punctuality of the Bosch delivery and the precise planning by Edtmayer the installation process went without a hitch